Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
 author
A mechanical seal for polymerizing fluids must manage more than pressure, speed, and chemical compatibility. In polymer, resin, latex, and other polymerizing pump services, product can accumulate around the seal faces or inside the seal chamber, while local frictional heat can make the buildup problem worse. Industry experience with polymer dispersions shows that material may preferentially adhere to warm seal surfaces and that frictional heat in the seal gap can promote particle agglomeration and disturb the sealing interface.
For maintenance and procurement teams, replacing a leaking seal with another unit of the same dimensions may therefore repeat the failure. The actual question is whether product contact, local heat, residence time, operating cycle, and the flush or support arrangement are creating an unfavorable environment around the seal.
Polymerizing-fluid pump service is different from handling a clean, stable liquid. A seal can fit the pump correctly yet develop deposits that interfere with lubrication or prevent normally moving components from responding to shaft and face movement.
Mechanical seal faces depend on a very thin fluid film. When polymerizing product accumulates at that interface, the deposit can change face contact, increase friction, or force the faces apart. A published polymer-dispersion pump case documented latex adhering to the warm seal faces and entering the sliding interface; frictional heat then contributed to polymer-particle agglomeration and eventual seal failure.
When a polymer pump seal leaks repeatedly, inspect where the deposit is concentrated. Heavy buildup directly on the faces suggests a different problem from a chamber filled with relatively uniform deposits. Face condition, discoloration, deposit thickness, and whether the faces still move freely can help determine whether heat and poor lubrication are contributing to the failure.
Polymer buildup does not have to damage the seal faces directly to cause leakage. Deposits around springs, dynamic O-rings, sleeves, or other compensating parts can restrict movement. Once the seal can no longer compensate for normal axial movement or face wear, stable face contact becomes more difficult.
This is why mechanical seal material selection matters but cannot be the only corrective action. XYM’s material guidance notes that deposits and solids may restrict secondary-seal movement, while temperature and lubrication affect face behavior and friction. A harder face material may resist wear, but it does not remove polymer from a stagnant cavity or restore a component that has been immobilized by deposits.
A common troubleshooting mistake is to look only at the process temperature shown on the operating sheet. The fluid at the seal faces may experience a different local thermal condition.
Mechanical seal faces generate friction during operation, and the local temperature also depends on lubrication, circulation, chamber geometry, and heat removal. A polymer-dispersion case showed that latex preferentially adhered to the warmest surfaces—the seal faces—even though the important failure mechanism was localized at the sealing interface rather than simply defined by bulk process temperature.
If polymer buildup is concentrated on the faces, maintenance teams should compare process temperature with any available seal-chamber or support-fluid temperature information. They should also check circulation and cooling condition rather than assuming that a normal bulk-fluid temperature rules out a thermal problem.
Polymer service can create a self-reinforcing failure sequence:
Poor face lubrication → higher friction → more local heat → more buildup or agglomeration → poorer face conditions → additional heat and leakage.
That does not mean every polymerizing product responds to temperature in the same way. Polymerization, coagulation, viscosity change, and deposit formation depend on the chemistry and operating environment. The practical objective is not simply to make the seal as cold as possible; it is to maintain a seal environment that supports lubrication without creating conditions that accelerate undesirable product buildup.
Before changing the seal design, determine where the polymer is forming and when the failure appears.
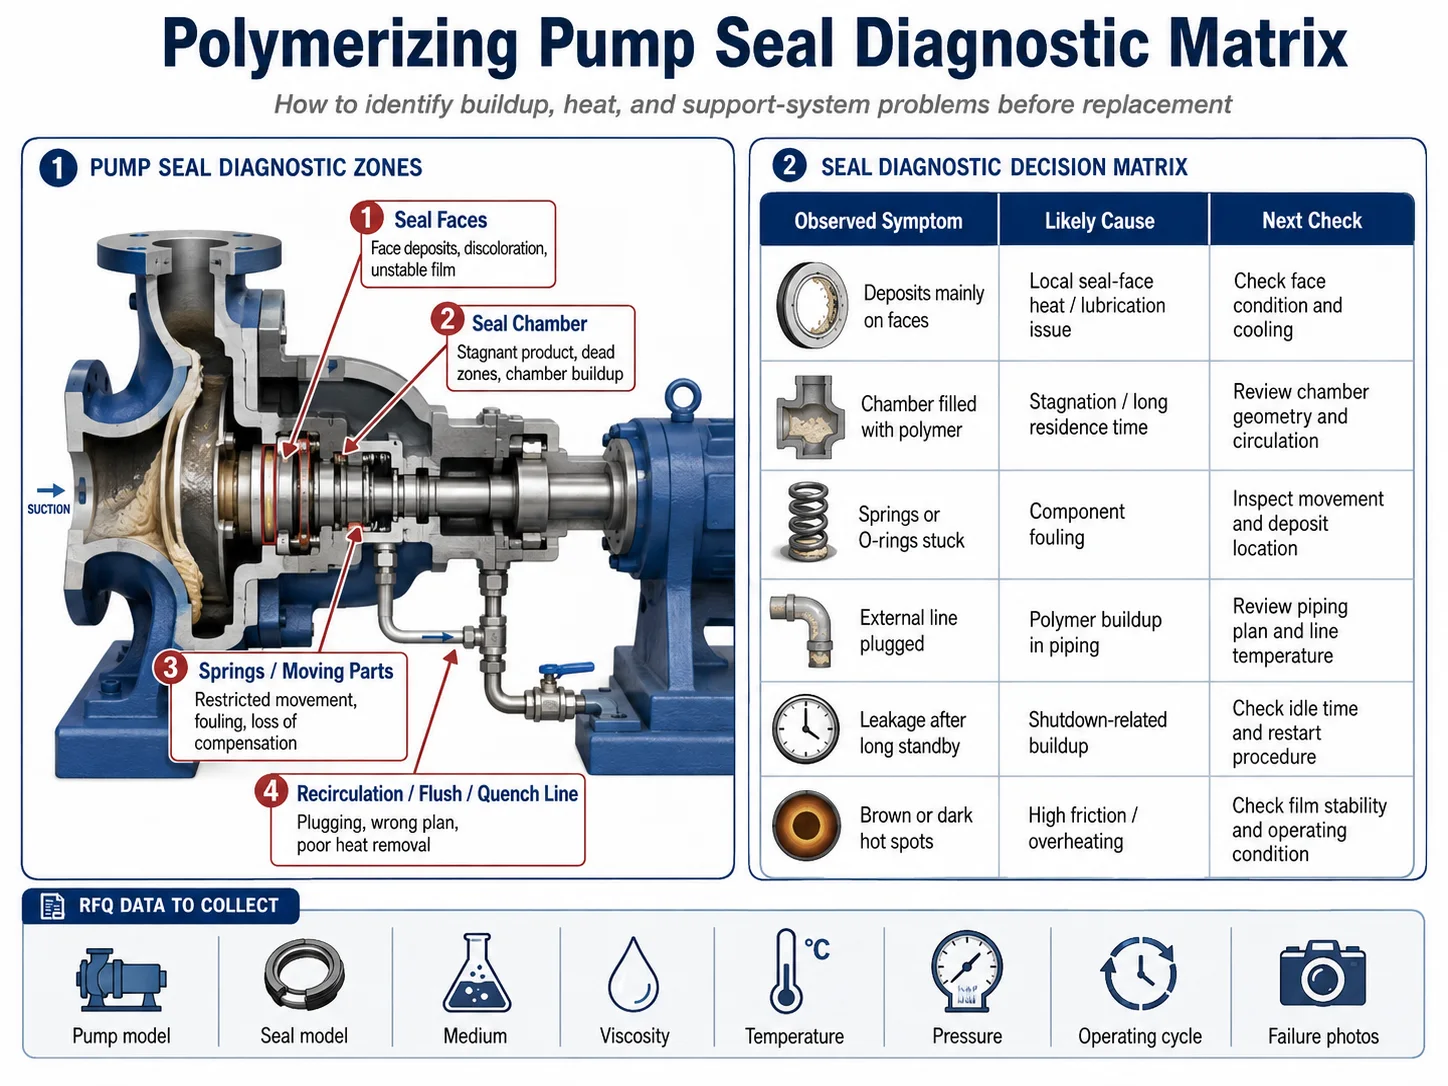
| Observation | More Likely Direction | Next Check |
|---|---|---|
| Heavy deposits concentrated on the faces | Local heat or lubrication problem | Face condition, temperature, fluid film |
| Seal chamber filled with deposits | Stagnation or long residence time | Chamber geometry and circulation |
| Springs or dynamic seals stuck | Compensation-system fouling | Component movement and deposit location |
| External recirculation line plugged | Polymer buildup in piping | Line temperature, orifice, residence time |
| Leakage mainly after long standby | Shutdown-related buildup | Residual product and restart procedure |
| Faces show abnormal heat discoloration | Friction or inadequate heat removal | Lubrication, cooling, operating condition |
This inspection should be done before ordering an identical replacement. Photographs of the deposit location and failed components can give the seal supplier substantially more useful information than a model number alone.
The mechanical seal and the chamber around it should be treated as one operating environment. XYM’s range of industrial pump mechanical seals covers different pump configurations, but selection still needs to be based on the medium, operating conditions, lubrication, heat, and actual failure pattern rather than shaft diameter alone.
A chamber that allows polymerizing product to remain relatively stagnant can create an unfavorable location for deposit formation. During a retrofit, the supplier should therefore review the seal-chamber dimensions and available circulation path, not just copy the old cartridge.
Purchasers should provide a chamber drawing where possible. If the existing cavity is heavily coated while the main process stream remains relatively clean, that difference is valuable diagnostic evidence and may indicate that residence around the seal deserves more attention.
Operating cycle matters. A continuously running pump can have a different thermal and circulation environment from a standby or batch-transfer pump that remains full of product for long periods.
Industry experience with polymer-dispersion pumps has required different sealing approaches for continuous and discontinuous duties, showing why operating mode should be included in the design basis. For an intermittent pump, specify normal run time, shutdown duration, whether the chamber remains filled, and what happens during restart.
The piping arrangement can be as important as the mechanical seal. Some plans introduce clean fluid into the chamber, while others recirculate process fluid or act only on the atmospheric side. They should not be treated as interchangeable.
An external clean flush can be considered when the objective is to remove heat and reduce the amount of polymerizing process fluid entering or remaining in the seal chamber. API Plan 32 uses a clean external source and is identified for applications including polymerizing or oxidizing fluids; its functions include heat removal and displacement of process material from the chamber. The injected fluid must remain compatible with the process.
The main purchasing question is whether process dilution is acceptable. If even a small amount of flush fluid affects product quality or downstream processing, the sealing strategy needs further review rather than automatically adding water or another clean liquid.
A piping plan that works well with a clean, stable liquid may be unsuitable for polymerizing service. External tubing and small control orifices add surfaces and residence time outside the pump, and those locations can themselves become fouling points.
Flowserve’s published piping-plan guidance identifies Plans 11 and 13 for clean, non-polymerizing fluids and lists clogged orifices as a typical maintenance concern. Its Plan 01 guidance also notes that internal circulation can reduce the risk of freezing or polymerizing material in exposed Plan 11 piping in suitable applications.
Therefore, a recurring plugged flush line should be treated as part of the root cause, not simply cleaned and returned to service indefinitely.
Plan 62 is a quench on the atmospheric side of a single seal. Industry guidance lists it for cases where outboard leakage may polymerize and where water, steam, or another suitable quench can reduce accumulation around the atmospheric side.
It is not the same as a process-side flush. If the polymer is building inside the seal chamber or between the inboard faces, adding a Plan 62 quench does not automatically remove that root cause. The quench medium must also be compatible with the application.
A double seal should be evaluated when the process needs a cleaner, more controlled sealing environment, when leakage consequences are significant, or when an external process-side flush would create unacceptable product dilution. Pressurized dual-seal support arrangements can isolate process fluid in suitable applications, and published piping-plan guidance includes polymerizing fluids among possible applications for some Plan 53 and Plan 54 systems.
However, a double seal is not an automatic cure. Barrier-fluid compatibility, contamination consequences, chamber design, pressure relationship, and polymer behavior still require review. For the broader arrangement decision, use single vs double mechanical seal selection to separate general seal-configuration questions from this polymer-specific failure analysis. XYM’s existing guide specifically identifies sticky, crystallizing, and polymerizing media as cases where double-seal arrangements may need evaluation.
Repeated failure often means the environment around the replacement seal did not change.
The new unit may still face the same local heat, stagnant chamber, blocked recirculation line, unsuitable shutdown procedure, or product deposits around moving components. The process itself may also have changed in concentration, viscosity, temperature, formulation, or operating cycle.
Before ordering another cartridge, compare the failed unit with current operating data. The root cause may require a different seal arrangement, chamber strategy, flushing approach, or operating procedure rather than another dimensional copy.
A useful inspection should record:
XYM’s pump-seal information likewise treats overheating, end-face wear, lubrication, cooling-system condition, and spring behavior as separate diagnostic areas rather than assuming every leak has the same cause.
For an application-based quotation, provide the pump manufacturer and model, existing seal model, shaft size, seal-chamber drawing, process medium, polymer or monomer information, concentration, viscosity, operating temperature, pressure, and speed.
Also provide any known polymerization, coagulation, or temperature sensitivity; continuous or intermittent duty; normal standby duration; existing flush or quench arrangement; product-dilution limits; failure photographs; deposit photographs; and required quantity.
Xinyoumi’s broader Xinyoumi mechanical seal solutions include pump mechanical seals and sealing auxiliary equipment, so supplying both mechanical and process information helps distinguish a standard replacement from an application that needs a revised sealing-system approach.
A supplier should be able to explain the failure mechanism behind the recommendation, not simply provide a chemically resistant seal.
A technically useful review should ask whether deposits appear mainly on the faces, inside the chamber, around springs, or in external piping. It should also consider whether failure occurs during continuous running, after shutdown, or during restart.
The supplier should ask about process temperature, operating cycle, lubrication, current flushing, dilution restrictions, and changes in formulation. Without this information, a recommendation based only on shaft size and previous material codes may repeat the same problem.
The quotation should identify the proposed seal arrangement, material direction, chamber assumptions, and any required flush, quench, barrier, cooling, or monitoring conditions. It should also distinguish confirmed application data from values still requiring customer verification.
For polymerizing pump service, Xinyoumi can evaluate the requirement within its existing pump-seal and auxiliary-equipment product scope, but the suitable configuration still depends on the submitted process and equipment data.
Mechanical seals for polymerizing pump service should be selected around the complete failure mechanism. Product buildup may originate at warm seal faces, in stagnant chamber areas, around moving components, or even inside external circulation piping. Local seal-face heat can contribute to the problem, but simply adding cooling, harder faces, or another replacement cartridge may not address the cause.
For a new selection or repeated failure review, prepare the pump model, seal and chamber dimensions, medium and concentration, viscosity, pressure, temperature, operating cycle, existing flush or quench arrangement, dilution restrictions, failed-seal photographs, deposit photographs, and target quantity. Buyers can contact Xinyoumi with this information for application review and quotation.
Polymerizing products may accumulate where local temperature, product contact, residence time, and fluid-film conditions favor deposit formation or agglomeration. Face deposits should be evaluated together with chamber and operating conditions.
It can contribute in some polymerizing systems. Published polymer-dispersion experience shows frictional heat in the seal gap contributing to polymer-particle agglomeration, but the effect depends on the chemistry and operating conditions.
There is no single plan for every application. Plan 32 may be considered when a compatible external clean flush can remove heat and process material, while some product-recirculation plans are specifically described for non-polymerizing fluids.
Plan 62 can help control accumulation caused by leakage on the atmospheric side of a single seal. It does not automatically solve polymer buildup inside the process-side seal chamber.
Provide pump and seal details, chamber dimensions, medium composition, viscosity, pressure, temperature, operating cycle, known polymer behavior, current flushing or quench arrangement, dilution limits, failure photographs, deposit evidence, and required quantity.